How boards are made
From raw substrate to finished panel
Production begins with substrate preparation: selecting and grading wood, conditioning it to a controlled moisture level, and sorting it by grain and thickness. Each stage narrows tolerance before the next begins.
Bonding, pressing, trimming, and surface leveling follow in sequence. The result is a dimensionally consistent veneer sheet, plywood, laminboard, or flush door ready for downstream use.
Production sequence
Veneer, layering, pressing, and trimming
01
Veneer peeling
Logs are peeled into continuous veneer, then cut to sheet size. Thickness is checked at intervals so each sheet falls within its specified range.
02
Layering and adhesive
Veneer plies are laid with alternating grain direction. Adhesive is applied evenly across each face to bond the layers without starved or excess glue lines.
03
Hot-press bonding
Layered assemblies enter a hot press under controlled temperature, pressure, and dwell time. The press cycle cures the adhesive and sets the panel flat.
04
Edge trimming and finish
Cured panels are trimmed to nominal dimensions, edges are squared, and surfaces are sanded and leveled for flush doors and board panels.
Calibration and control
Thickness regulation and inspection
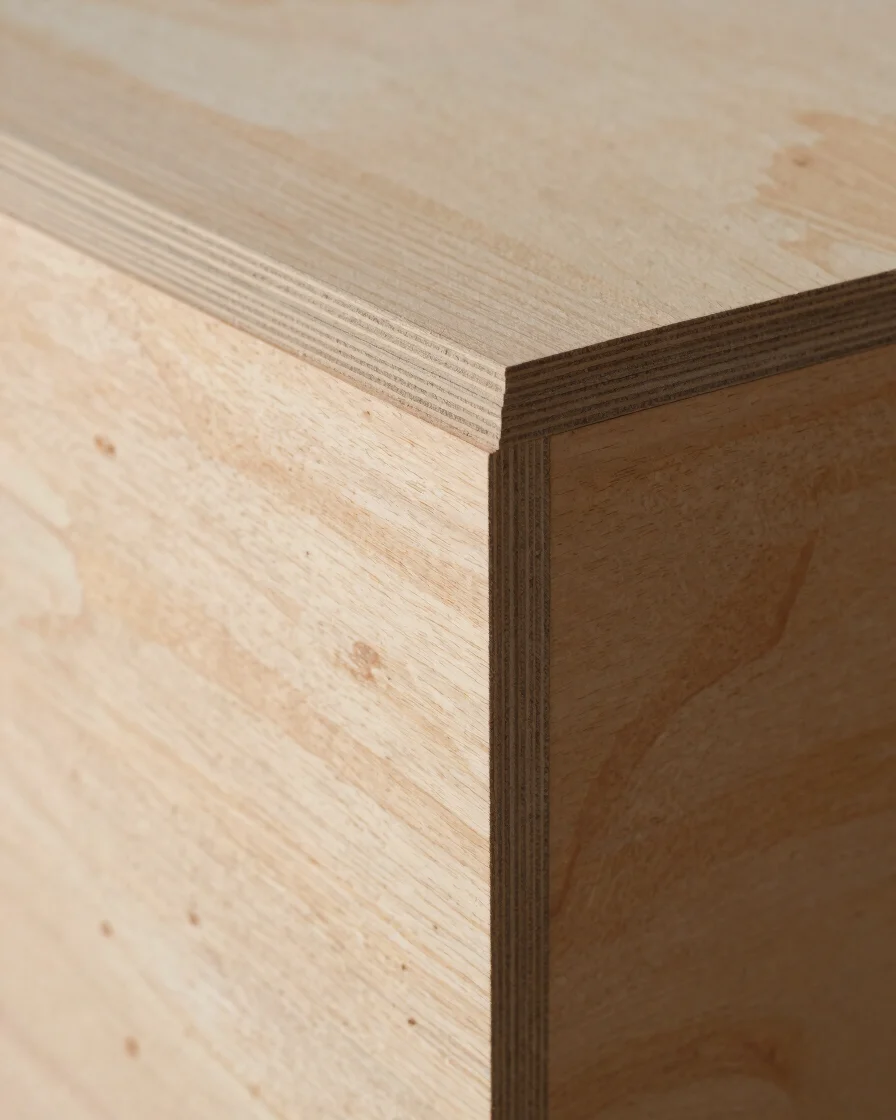
Board calibration sets thickness across the line, with sanding and leveling passes adjusted to the target dimension. Measurements are taken at defined points so drift is caught before a batch leaves the line.
Quality control inspects bonding, edge squareness, and surface flatness against the stated specification. Batches that fall outside tolerance are held back for review rather than shipped.